Business Details
Industrial Pump Manufacturer for OEM Solutions
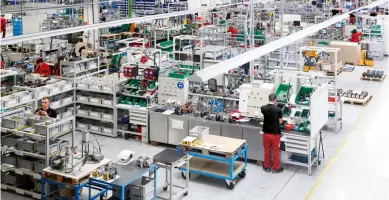
Speck Industries, a wholly-owned subsidiary of Speck Pumps based in Roth, Germany, has dedicated over a century to designing and manufacturing industrial OEM pumps. Our expertise spans regenerative turbine, centrifugal, side channel, liquid ring vacuum, and positive displacement pump technologies, engineered to meet the most demanding applications in corrosive environments, temperature extremes, and high-vacuum conditions. With a global presence and a US facility serving North America, we combine family-owned tradition with cutting-edge innovation to deliver customized fluid handling solutions. Our commitment to quality is underscored by DIN EN ISO 9001 certification, ensuring rigorous standards across 10,000 sq. ft. of modern, automated production space.We specialize in solving complex challenges for industries including medical technology, chemicals, pharmaceuticals, and general manufacturing, supported by a team of 560 professionals dedicated to technical excellence and client collaboration.
Services
Centrifugal Pump Design
Vacuum Pump Systems
Regenerative Turbine Pumps
OEM Pump Manufacturing
Fluid Handling Solutions
Highlights and features
- We offer 100+ years of specialized expertise in industrial pump engineering.
- Our ISO 9001-certified processes ensure uncompromising quality standards.
- We provide customized pump solutions for extreme operating conditions.
- Our global manufacturing capabilities support both one-off and large-scale production.
- We maintain 10,000 sq. ft. of advanced US-based production and logistics facilities.
Associations and certifications
- ISO 9001
Services
Centrifugal Pumps
Our centrifugal pumps deliver high-reliability fluid transfer solutions for flow rates exceeding 2000 GPM. Engineered with stainless steel and ductile iron components, these pumps operate efficiently in temperatures up to 660F while maintaining NPSH inducer stages for challenging suction conditions. Applications include hot oil transfer, boiler feed systems, and pharmaceutical process heating.
Vacuum Pump Systems
We design liquid ring vacuum systems capable of achieving 29 in-Hg vacuum levels with flow capacities from 32 to 1200 CFM. These corrosion-resistant systems utilize advanced sealing technologies and ATEX-compliant designs for hazardous environments, serving applications in chemical processing and industrial vacuum requirements.
Regenerative Turbine Pumps
Our regenerative turbine pumps provide compact high-pressure solutions with exceptional vapor handling capabilities. Constructed from stainless steel and brass, these pumps operate effectively in temperatures up to 660F with magnetic drive or mechanical seal options, ideal for microchip manufacturing chillers and beverage bottling systems.
OEM Pump Design
We offer complete OEM pump design services from concept to production, including mechanical and electrical design, firmware development, and prototype testing. Our engineers optimize pump configurations for specific applications involving thermal extremes, chemical resistance, and unique power requirements.
Industrial Fluid Handling
Our industrial fluid handling solutions address challenging applications including liquefied gas transfer, high-viscosity fluid pumping, and extreme ambient condition operations. With sealing options ranging from mechanical seals to magnetic couplings, we ensure reliable performance in temperatures from -100C to 430C.
Questions
What types of pumps does Speck Industries manufacture?
We produce centrifugal, regenerative turbine, side channel, gear, rotary vane, oscillating piston, and liquid ring vacuum pumps for industrial applications.
Can Speck develop custom pump solutions?
Yes, we specialize in modifying standard pumps or designing new systems tailored to specific operational requirements and environmental conditions.
What industries use Speck pump systems?
Our pumps serve medical technology, chemical processing, pharmaceutical production, energy systems, and general industrial fluid transfer applications.
What quality certifications does Speck hold?
We maintain DIN EN ISO 9001 certification for our quality management systems across global production facilities.
What materials are used in Speck pumps?
We utilize stainless steel, bronze, ductile iron, cast iron, and polymers to ensure chemical resistance and durability in extreme conditions.