Business Details
34 Years
experience
Custom Engineered Conveyor Systems for Material Handling
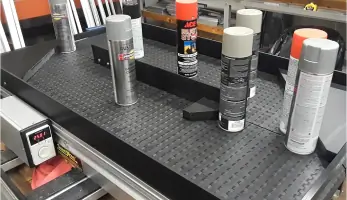
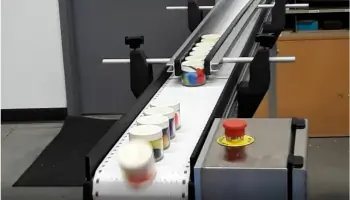
Our company designs and manufactures conveyor systems in the USA, delivering fully customized solutions built to exact specifications. We pride ourselves on rapid engineering timelines, producing systems in a matter of days without compromising quality or performance. Each conveyor arrives ready for immediate use and is designed for simple assembly without the need for installers or service technicians. By focusing on efficient design and modular construction, we help customers quickly implement reliable material handling systems that support their operational goals.We manufacture solid-surface workstation conveyors that promote safety, cleanliness, and efficiency across a wide range of applications. Available configurations include straight or extended lines, multi-level systems, accumulation, spacing, batch counting, carousel layouts, and integrated weigh scales. Our workflow automation technology is customized to your production line at no additional cost, ensuring optimal performance. Our modular ESD plastic chain conveyors are quiet, clean, and maintenance-free, making them ideal for daily assembly and packaging tasks. Systems can be expanded easily by adding components, and optional casters allow for portability. Each conveyor uses an energy-efficient 25-watt drive compatible with standard 120V outlets and includes safety belting that separates during jams or overloads. Built to order and shipped quickly, our systems are designed to keep operations moving.
Services
Modular Conveyors
Custom Engineered Systems
Pharmaceutical Conveyors
90 Degree Turn Conveyors
Accumulation Conveyors
Multi-Lane Systems
Incline Conveyors
Food Industry Conveyors
Robotic Interface Units
Washdown-Ready Systems
Details
- Year established: 1992
Highlights and features
- We engineer custom conveyor systems to exact specifications within days.
- Our plug-and-play systems require no technicians for installation.
- Snap-link belting prevents injuries during overloads or jams.
- Energy-efficient motors use less than 2 amps per unit.
- Manufactured in the USA with FDA-approved materials.
Services
Modular Conveyors
SmartMove's modular conveyors offer adaptable configurations for diverse applications. These systems feature snap-link ESD plastic belting and lightweight aluminum frames, enabling rapid reconfiguration for changing production needs. The modular design reduces downtime during expansions or modifications while maintaining structural integrity across industries like pharmaceuticals and automotive manufacturing.
Pharmaceutical Conveyors
Specialized conveyor solutions for pharmaceutical environments combine FDA-approved materials with sanitary designs. Systems include recessed workstations, washdown capabilities, and precise batch-counting features. The conveyors maintain product integrity through contamination-resistant surfaces and controlled accumulation processes tailored to drug manufacturing and packaging requirements.
90 Degree Turn Conveyors
Engineered for space optimization, these conveyors enable seamless product redirection without manual intervention. The systems maintain consistent throughput at 138 feet per minute while handling diverse loads from small parts to 50lb boxes. Integrated guide rails ensure product stability during directional changes in packaging and assembly applications.
Accumulation Conveyors
SmartMove's accumulation conveyors manage product flow with zero-pressure accumulation technology. These systems organize items for packaging, sorting, or order fulfillment while preventing damage through controlled spacing. Available in multi-lane configurations, they integrate with automated processes for industries requiring high-volume material handling.
Robotic Interface Conveyors
Conveyor systems designed for robotic integration support collaborative workflows between automated arms and material transport. Features include synchronized speed control, sensor-triggered stops, and modular mounting options. These systems enhance precision in applications like CNC machine tending and robotic pick-and-place operations across manufacturing sectors.
Questions
What industries do SmartMove conveyors serve?
SmartMove serves pharmaceutical, automotive, electronics, food processing, cosmetics, medical, and hardware industries with customized material handling solutions.
Are SmartMove conveyors truly maintenance-free?
Yes, our modular systems with snap-link belting require no lubrication and minimal upkeep, designed for long-term reliability.
How quickly can I get a custom conveyor system?
Systems are engineered to specifications within days and shipped rapidly, with pre-assembled components for immediate installation.
Do conveyors work with robotic systems?
Yes, our systems integrate seamlessly with robotic automation, including Kawasaki Delta Robots and custom robotic interfaces.
Are SmartMove conveyors energy efficient?
Our systems use under 2 amps per unit with low-voltage motors, reducing operational costs while maintaining high performance.
Videos
Reviews (3)
Rich Matthes
May 27, 2024
Report
SmartMove Conveyor is a quiet, efficient, versatile conveyor that can be used in a multitude of applications. SmartMove Conveyor is priced competitively with the market. SmartMove Conveyors service is excellent and ordering is very easy. SmartMove Conveyors products are shipped quickly and arrive well packaged and ready for a quick, easy installation. Overall, SmartMove is a great company to deal with and has fantastic products.
Ritchie Arney Globalmed Inc
Apr 23, 2019
Report
SmartMove provides conveyors and accessories promptly at a fair price, with excellent after sales follow ups. The quality and simplicity are excellent. We have already experienced significant production increases. Purchasing your conveyors was for us, a very Smart Move!
Mike Lettmoden
Oct 11, 2017
Report
Our SmartMove system was installed when we originally moved into the pharmacy in 2006. We are a long term care pharmacy and our daily operations last about 12 to 14 hours a day 6 days a week. Our conveyor belt runs non-stop all day every day, and has done so for almost 10 years now silently, smoothly and consistently. It is an integral part of daily operations and would triple our work load without having this pharmaceutical conveyor system. It has quite simply been the most reliable asset in the pharmacy for the past 10 years. Very few products can claim that kind of reliability.